Condition-Based Maintenance: When Equipment Condition Should Determine the Maintenance Intervention
The calendar can tell you when maintenance was scheduled. Equipment condition can help tell you when maintenance is actually needed.
For decades, industrial maintenance programs have relied heavily on time-based or usage-based interventions: inspect every three months, replace every 5,000 operating hours, overhaul annually, lubricate every predetermined number of weeks.
These strategies remain appropriate for many assets and failure modes.
But they also have an important limitation:
Equipment does not necessarily degrade according to the calendar.
Two identical machines operating in the same facility may experience very different degradation rates because of load, operating environment, installation quality, lubrication, contamination, process conditions, duty cycle, alignment, temperature, maintenance history and other factors.
This is where Condition-Based Maintenance (CBM) becomes strategically important.
Rather than intervening simply because a predetermined interval has expired, CBM uses evidence about the actual condition of the asset to help determine whether maintenance should be performed, planned, intensified, deferred or further investigated.
The objective is not to eliminate scheduled maintenance.
The objective is to make maintenance decisions that better reflect how the equipment is actually behaving.
From Calendar-Based Maintenance to Condition-Based Decisions
Traditional preventive maintenance generally asks:
“Is it time to perform the maintenance task?”
Condition-Based Maintenance asks a different question:
“Does the current condition of the equipment indicate that intervention is necessary?”
That distinction can fundamentally change maintenance planning.
Consider a critical rotating asset scheduled for overhaul every 12 months.
At month twelve, condition indicators may show stable vibration, acceptable lubricant condition, normal operating temperatures and no meaningful deterioration in performance.
Another identical asset may begin showing increasing vibration, lubricant contamination and temperature changes only six months after its previous intervention.
A rigid calendar treats those assets similarly.
A condition-based strategy recognizes that their maintenance requirements may no longer be the same.
Asset ConditionDegradation DetectionTechnical InterpretationMaintenance DecisionPlanned Intervention
This is the foundation of CBM.
Condition-Based Maintenance Is More Than Monitoring
One of the most common misconceptions in industrial maintenance is that installing sensors automatically creates a Condition-Based Maintenance program.
It does not.
A facility may collect enormous quantities of vibration, temperature, pressure, electrical and process data without actually practicing effective CBM.
Monitoring produces information. CBM converts relevant condition information into maintenance decisions.
A mature CBM process therefore requires more than instrumentation.
It requires understanding:
- what function the asset must perform;
- how that function can fail;
- which failure modes develop progressively;
- which physical parameters change as degradation develops;
- whether those changes can be detected reliably;
- how much warning time exists;
- what level of deterioration requires action;
- and what maintenance response is technically and economically justified.
Without this logic, organizations risk creating sophisticated monitoring systems that generate alarms without improving maintenance effectiveness.
The Failure Mode Must Come First
The starting point for CBM should not be the sensor.
It should be the failure mode.
This connects Condition-Based Maintenance directly with FMEA, FMECA and Reliability-Centered Maintenance principles.
Required FunctionFunctional FailureFailure ModeDetectable ConditionMonitoring MethodMaintenance Decision
For example, installing vibration monitoring on a pump only creates value if the vibration characteristics being measured can provide meaningful information about relevant degradation mechanisms such as:
- bearing deterioration;
- misalignment;
- imbalance;
- looseness;
- mechanical resonance;
- cavitation;
- or other identifiable mechanical conditions.
The same principle applies across other technologies.
Do not select the monitoring technology first and then search for something to measure.
Identify the relevant failure mode first.
Then determine whether there is a technically credible way to detect its development early enough to act.
What Conditions Can Be Monitored?
Industrial assets communicate their condition through multiple physical and operational parameters.
Depending on the equipment and failure mechanism, useful indicators may include:
Vibration
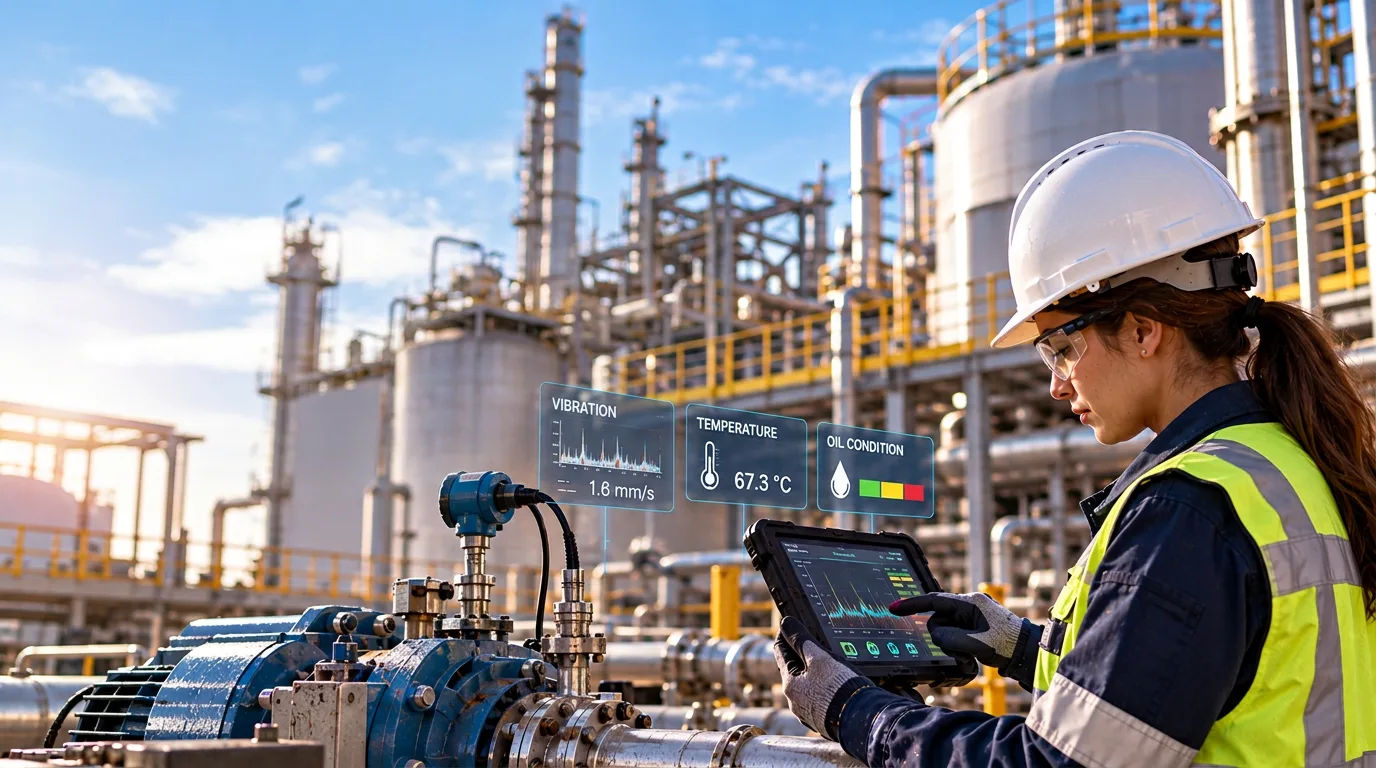
Vibration analysis can provide valuable information about the mechanical condition of rotating equipment such as motors, pumps, compressors, turbines, fans and gearboxes.
Changes in amplitude, frequency content and vibration patterns can help identify developing mechanical abnormalities.
Temperature
Abnormal temperature patterns may indicate friction, inadequate lubrication, electrical resistance, insulation problems, process abnormalities, overloaded components or deteriorating mechanical conditions.
Thermography and installed temperature instrumentation can therefore support condition assessment across mechanical and electrical systems.
Lubricant and Oil Condition
Lubricants can carry valuable evidence about what is occurring inside equipment.
Particle contamination, wear debris, viscosity changes, water contamination and other lubricant characteristics can provide insight into both lubricant health and equipment condition.
Ultrasound
Ultrasonic inspection can support detection of conditions such as compressed-air or gas leakage, steam-trap abnormalities, electrical discharge and certain mechanical or lubrication-related conditions.
Electrical Condition
Motors and electrical equipment can be evaluated through parameters such as current, insulation condition, temperature, electrical signature and other diagnostic indicators.
Process and Performance Data
Some of the most valuable condition indicators already exist inside the process control environment.
Pressure. Flow. Temperature. Power consumption. Efficiency. Speed. Output. Differential pressure.
A machine does not necessarily have to exhibit obvious mechanical symptoms before its performance begins to deteriorate.
This makes process data an important part of the CBM architecture.
A Single Reading Is Rarely the Whole Story
Condition-Based Maintenance becomes significantly more powerful when organizations move from isolated readings to trend analysis.
One vibration reading may indicate that a machine is currently above or below a threshold.
A sequence of readings may reveal something more important:
the direction and rate of deterioration.
The same principle applies to temperature, lubricant condition, pressure, efficiency and other parameters.
BaselineTrendDeviationDiagnosisDecision
This is why historical data matters.
The question is not always:
“Is this measurement bad?”
Sometimes the more important question is:
“How quickly is this condition changing?”
An asset approaching an alarm threshold rapidly may require more attention than another asset operating at a higher but stable level.
Engineering interpretation remains essential.
The P–F Interval: Creating Time to Act
A central concept behind effective Condition-Based Maintenance is the P–F interval.
P represents the point at which a developing failure becomes potentially detectable.
F represents functional failure — the point at which the asset can no longer perform its required function to the necessary standard.
Between those points exists an opportunity.
Potential FailureDetectable DegradationWarning TimePlanned InterventionFunctional Failure
The objective of condition monitoring is not merely to discover that equipment is deteriorating.
It is to discover that deterioration early enough to make a better maintenance decision.
That warning time may allow the organization to:
- confirm the diagnosis;
- increase monitoring frequency;
- evaluate operational risk;
- order materials;
- secure spare parts;
- coordinate production;
- prepare permits;
- schedule technicians;
- develop the work package;
- and execute maintenance under controlled conditions.
This is where CBM can transform an unexpected failure into a planned maintenance event.
Monitoring Frequency Must Match Failure Behavior
A technically appropriate monitoring technology can still fail as a maintenance strategy if the inspection interval is wrong.
If a failure can progress from detectable degradation to functional failure in three weeks, collecting condition data every three months provides little protection.
Monitoring Interval < Useful P–F Interval
The exact relationship depends on the failure mechanism, technology, asset criticality, operating context and required response time.
Failure BehaviorDetectabilityP–F IntervalMonitoring FrequencyPlanning Window
Monitoring frequency should not be selected simply because “monthly vibration routes” or “quarterly thermography” have always been performed.
The interval should reflect the behavior of the failure being managed.
Not Every Failure Mode Is Suitable for CBM
Condition-Based Maintenance is powerful, but it is not universally applicable.
Some failure modes:
- provide little or no detectable warning;
- progress too rapidly;
- are difficult to monitor reliably;
- have monitoring costs disproportionate to their consequences;
- or are better managed through another maintenance strategy.
In those situations, the appropriate response may be:
- scheduled preventive replacement;
- functional testing;
- proof testing;
- redesign;
- improved operating procedures;
- redundancy;
- protective systems;
- spare-parts strategy;
- or controlled run-to-failure.
The most technologically advanced maintenance strategy is not automatically the best strategy.
The correct strategy is the one that appropriately manages the relevant failure mode and its consequences.
CBM Does Not Mean “Wait Until the Equipment Is Bad”
Another misconception is that Condition-Based Maintenance means allowing equipment to deteriorate until failure is imminent.
That is not the objective.
A mature CBM program establishes decision criteria before the condition becomes unacceptable.
Normal Condition
Continue operation and routine monitoring.
Developing Deviation
Increase monitoring frequency and investigate.
Confirmed Degradation
Plan maintenance intervention.
Severe Condition
Evaluate immediate operational risk and determine whether continued operation is acceptable.
The purpose is controlled decision-making.
Not delayed maintenance.
Asset Criticality Changes the Decision
Condition data should never be interpreted independently from asset criticality.
The same abnormal condition may justify different actions on different assets.
Consider two similar pumps.
Pump A has full installed redundancy and can be isolated without affecting production.
Pump B has no operational spare and its failure could stop a critical process.
Both may show similar developing bearing degradation.
But the business consequence is different.
Equipment Condition + Asset Criticality + Failure Consequence = Maintenance Priority
This is where CBM connects directly with the broader reliability strategy.
Condition tells us what may be happening to the asset.
Criticality tells us how much that condition matters to the operation.
Both are necessary.
Avoid the Alarm Trap
Digital monitoring systems can generate hundreds or thousands of alarms.
More alarms do not necessarily create better reliability.
Poorly designed thresholds can produce alarm fatigue, unnecessary work orders and loss of confidence in the monitoring system.
DataInformationDiagnosisDecisionAction
Not every deviation requires maintenance.
Not every alarm represents failure.
And not every abnormal condition requires immediate shutdown.
The purpose of CBM is not to create more work.
It is to create better work at the right time.
Condition-Based Maintenance and the CMMS
For CBM to influence execution, condition information must eventually connect with the maintenance management system.
Condition MonitoringTechnical AnalysisMaintenance RecommendationCMMS Work OrderPlanning & SchedulingExecutionVerification
This creates traceability between the detected condition and the maintenance response.
The CMMS can then preserve valuable history:
- condition findings;
- failure codes;
- maintenance recommendations;
- work performed;
- parts replaced;
- inspection results;
- post-maintenance condition;
- and recurring equipment problems.
Over time, this information helps organizations improve both maintenance strategy and equipment reliability.
CBM Must Be Closed-Loop
One of the most overlooked steps occurs after maintenance has been completed.
Was the diagnosis correct?
Did the intervention eliminate the abnormal condition?
Did vibration return to baseline?
Did temperature normalize?
Did equipment performance recover?
Were the suspected components actually degraded?
Without verification, organizations lose an important learning opportunity.
DetectDiagnoseDecidePlanInterveneVerifyLearn
This feedback loop improves future diagnosis, alarm thresholds, maintenance tasks and failure-mode knowledge.
CBM should therefore become a learning system, not merely an inspection program.
The Economic Question Still Matters
Condition monitoring should create operational value.
Not every asset justifies permanent sensors, advanced analytics or continuous monitoring.
The business case should consider:
- asset criticality;
- failure consequences;
- failure frequency;
- monitoring cost;
- inspection accessibility;
- cost of downtime;
- available redundancy;
- repair lead time;
- spare-parts availability;
- and the economic value of additional warning time.
For some critical assets, continuous monitoring may be justified.
For others, periodic portable measurements may be sufficient.
For low-consequence equipment, sophisticated CBM may create little economic benefit.
Technology intensity should follow risk and value — not enthusiasm for technology.
From Maintenance Activity to Maintenance Intelligence
The strategic value of Condition-Based Maintenance extends beyond individual inspections.
When implemented correctly, CBM helps organizations transition from:
Fixed Maintenance Intervals
to:
Condition-Informed Maintenance Decisions
And eventually toward:
Risk-Informed Asset Management
The evolution can be represented as:
Asset CriticalityFailure ModeCondition IndicatorMonitoringTechnical InterpretationMaintenance DecisionPlanned InterventionVerificationReliability
That is a much stronger architecture than simply collecting more equipment data.
The Human Factor Still Matters
Artificial intelligence, automated diagnostics, wireless sensors and advanced analytics will continue to expand the capabilities of industrial condition monitoring.
But technology does not eliminate the need for engineering judgment.
Someone still needs to understand:
What does this signal mean?
Is the condition actually deteriorating?
What failure mode could explain it?
How quickly is it progressing?
What happens if the asset continues operating?
What maintenance action is justified?
And when should that action occur?
Sensors detect signals. Systems organize data. Engineering judgment turns information into decisions.
That human layer remains fundamental.
The TLBS Perspective
At TLBS Corporation — Engineering, Projects & Maintenance, we view Condition-Based Maintenance as part of a broader reliability decision process.
The objective is not simply to inspect more equipment or install more sensors.
The objective is to understand the relationship between:
Asset CriticalityFailure ModeEquipment ConditionOperational ConsequenceMaintenance Decision
When those elements are connected, maintenance teams can focus technical resources where they create the greatest operational value.
Condition monitoring becomes more than inspection.
It becomes maintenance intelligence.
A Strategic Question for Industrial Leaders
Ask your maintenance and reliability organization:
“Are we intervening because the equipment condition justifies the work — or simply because the calendar says it is time?”
For some assets, the calendar will remain the correct trigger.
For others, actual equipment condition can provide a more intelligent basis for intervention.
The challenge is knowing the difference.
Final Perspective
Condition-Based Maintenance does not mean eliminating preventive maintenance.
It does not mean installing sensors everywhere.
And it does not mean waiting until equipment is close to failure.
It means using credible evidence about equipment condition to improve the timing and quality of maintenance decisions.
The strongest CBM programs connect failure modes, detectability, asset criticality, monitoring technology, engineering judgment and disciplined execution.
Because ultimately, the objective is not more data.
It is not more alarms.
And it is not more maintenance.
The objective is better maintenance decisions — made early enough to protect reliability, availability and operational continuity.
Understand the condition.
Understand the consequence.
Then decide when to intervene.
TLBS Corporation
Engineering, Projects & Maintenance